China Top Custom Aluminum Tri Fold Blind Rivets Suppliers
China’s manufacturing base gives buyers a broad field of fastener suppliers, but supplier count alone says little about quality. Custom Aluminum Tri-Fold Blind Rivets are designed to form a multi-fold blind-side bulb, helping secure assemblies where access is available from one side. Their performance depends on more than the rivet’s name: alloy, grip range, hole size, mandrel design, and installation tool all matter. A poor match may leave a loose joint or damage thin sheet.
Material scale provides useful context, not a demand forecast. The U.S. Geological Survey’s Mineral Commodity Summaries 2025 estimates global primary aluminum production at about 72 million metric tons in 2024. That figure describes primary metal, not rivets, and should not be treated as proof of any supplier’s capacity. Buyers comparing China-based manufacturers should request drawings, sample parts, dimensional inspection records, and clear production tolerances. Ask how the supplier controls forming consistency and verifies installation performance across the specified grip range. Look closely at the flange and formed bulb. Small details matter. A sample that works once is not enough; repeatable results across a production batch matter more. This guide examines supplier selection, customization, quality checks, and practical sourcing questions. There is no single best supplier for every application, and that is worth remembering.
What Defines a Tri-Fold Blind Rivet: 3 Legs, Body, and Mandrel
China Top Custom Aluminum Tri Fold Blind Rivets Suppliers
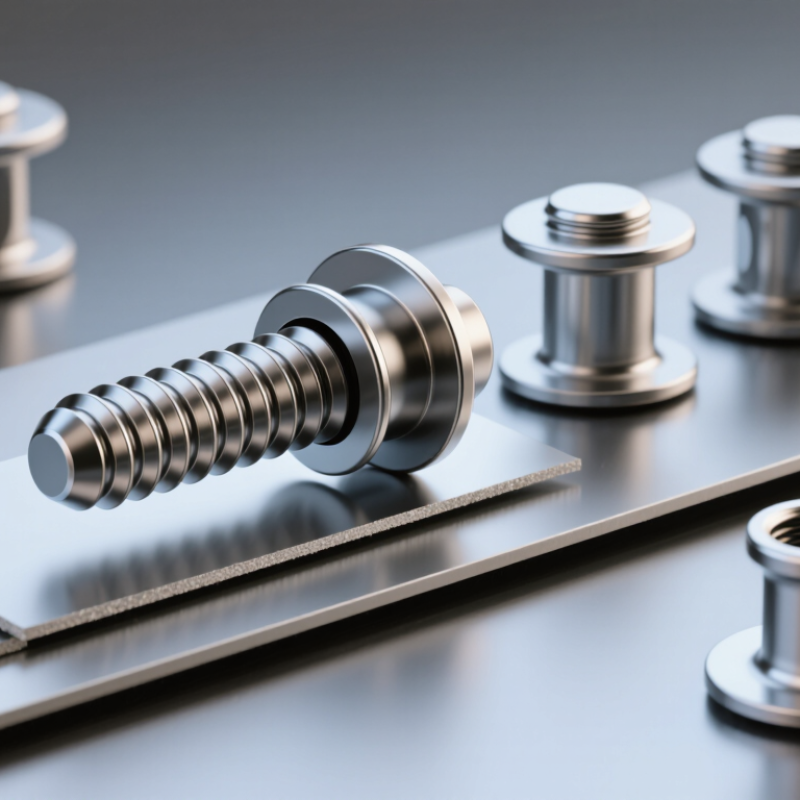
A tri-fold blind rivet has three working parts: a tubular body, a mandrel, and a body that splits into three legs during setting. The mandrel is pulled through the body. Its head expands the blind end, folding the legs outward against the rear surface. The result is a wider bearing area than a conventional blind rivet can provide. Three legs matter. They help distribute pressure across thin sheet or softer materials, though poor hole sizing can still cause loose joints or surface damage.
The mandrel does not remain intact: it breaks at a designed point after forming the legs. Its break load and the rivet’s grip range therefore deserve attention, not just body diameter. ISO 14589:2000 specifies mechanical tests for blind rivets, including tensile, shear, and mandrel break-load testing. Ask suppliers for test results matched to the selected material and grip range. NASA’s Fastener Design Manual also stresses selecting fasteners around joint loads and installation conditions. One useful material context: the USGS Mineral Commodity Summaries 2024 reports about 70 million metric tons of global primary aluminum production in 2023. That figure describes the wider aluminum supply, not rivet quality—a distinction worth keeping clear. Inspect samples for even leg spread, clean breaks, and a seated head. Real joints can be less tidy than diagrams.
China Top Custom Aluminum Tri Fold Blind Rivets Suppliers - What Defines a Tri-Fold Blind Rivet: 3 Legs, Body, and Mandrel
| Feature | Typical Construction or Data | Function in the Joint | Selection or Inspection Point |
| Three folding legs | The rivet body splits and folds into three legs on the blind side as the mandrel is pulled. | Creates a broad, three-point bearing area behind the workpiece. | Check that the legs form evenly and sit flat against the rear surface. |
| Rivet body | Commonly made from aluminum alloy for lightweight fastening; the body includes the head and expandable shank. | Passes through the prepared hole and expands to clamp the materials together. | Match body material and head style to the application, workpiece materials, and exposure conditions. |
| Mandrel | A pull stem, often made from steel in aluminum-body blind rivets, with a shaped head that drives the body to fold. | Applies the setting force and typically breaks at a designed point after installation. | Confirm the specified mandrel material and break performance; avoid assuming it matches the body material. |
| Rivet diameter | Selected to suit the joint design and the prepared-hole size. A 4.8 mm nominal rivet is one common size category. | Determines the fastener’s fit in the hole and contributes to joint capacity. | Use the supplier’s hole-size recommendation for the exact rivet; nominal diameter alone does not define the drill size. |
| Grip range | The stated total thickness of material that a particular rivet can clamp; the range varies by diameter and body design. | Allows the rivet to form correctly across the joined material stack. | Measure the combined material thickness and choose a rivet whose published grip range includes it. |
| Head style | Common options include dome, large-flange, and countersunk heads. | Provides the visible bearing surface on the accessible side of the joint. | Choose according to bearing-area needs, appearance, and whether the installation surface is prepared for a flush head. |
| Workpiece suitability | Tri-fold designs are used where the blind-side legs can expand and where a broad rear bearing area is useful. | Helps retain sheet materials or components when only one side of the joint is accessible. | Check rear-side clearance and material compatibility; the folded legs need room to form. |
| Installation check | Install with a compatible blind-rivet tool and the correct nosepiece for the rivet specification. | Applies a controlled pull to form the legs and complete the setting operation. | Inspect for a seated head, formed legs, and a clean mandrel break; follow the fastener and tool instructions. |
Note: Construction details, available sizes, hole recommendations, grip ranges, and load ratings vary by rivet design. Consult the product specification for the exact application.
Aluminum Alloy and Mandrel Choices for Corrosion Compatibility
Tri-fold blind rivets spread their legs behind thin or uneven panels, making alloy choice important to both grip and corrosion performance. For custom orders, suppliers should confirm the rivet body alloy, sheet materials, panel thickness, and exposure conditions. A rivet used on an indoor cabinet faces a different environment from one exposed to coastal spray. Details matter.
The mandrel deserves equal attention. An aluminum mandrel can improve material compatibility, but its strength must suit the installation load. Steel or stainless-steel mandrels may offer different strength and forming behavior, yet dissimilar metals can create a corrosion risk when moisture bridges the joint. The retained mandrel and surrounding body should be assessed as a system, not as separate parts. Not always obvious.
In practice, ask for material specifications and sample assemblies before approving a large production run. Check the joint after setting for clean leg formation, firm clamping, and any visible coating damage. Where salt, condensation, or cleaning chemicals are present, representative exposure testing can reveal problems that a catalog description will miss. I have seen a tidy material table leave out the actual panel alloy; that small omission can undermine an otherwise careful selection.
How 3.2, 4.0, and 4.8 mm Rivet Diameters Match Grip Ranges
China Top Custom Aluminum Tri Fold Blind Rivets Suppliers
Choosing a 3.2, 4.0, or 4.8 mm tri-fold rivet starts with the material stack, not the hole alone. Diameter describes the rivet body; it does not set the grip range. Grip range depends on the rivet’s length and design, so check the supplier’s specification chart for the exact part.
That’s the key.
A 3.2 mm rivet often suits lighter assemblies, such as thin sheet and small plastic panels, when the hole and load requirements permit. A 4.0 mm size can offer a practical middle ground for general panel work. A 4.8 mm rivet may suit thicker stacks or applications needing a larger body, provided the joint design supports it.
These are tendencies, not rules. Tri-fold legs spread behind the workpiece, which can help distribute pressure on softer materials.
Measure the combined thickness at the joint, including coatings or washers, then match it to the specified grip interval. If the stack sits below the minimum or above the maximum, the rivet may not form correctly. Check hole diameter, too; an oversized hole can leave a loose joint.
I still test a sample on the actual materials. Charts help, but they cannot show every real-world fit. A slightly uneven fold can be easy to miss during a quick visual check.
Which Tests Measure Rivet Pull Force, Shear Strength, and Leg Deployment?
China Top Custom Aluminum Tri Fold Blind Rivets Suppliers
Rivet performance needs separate tests; one force reading cannot describe every failure mode. ISO 14589:2000, Blind rivets—Mechanical testing, provides methods for assessing tensile and shear strength. In a tensile test, pull the set rivet along its axis and record the peak load. For shear strength, load overlapping sheets parallel to their joint, then record the load at failure. These values depend on rivet diameter, alloy, grip range, and sheet thickness. Compare like with like. Installation pull force is not the same as the finished joint’s pull resistance.
Leg deployment needs its own setting check. Install samples in the actual material stack, then inspect the blind side. A well-set tri-fold rivet should show three evenly formed legs, firm contact, and no crushed or missing leg. Record deployment appearance, setting force, grip thickness, and any head lift. ISO 14589 supports mechanical testing, but visual or sectioned inspection helps assess leg formation. Small details matter. A batch report should state sample count, peak loads, test setup, and failure mode; averages alone can hide weak specimens.
Tips: Test across the intended grip range, not just one thickness. Photograph the formed legs beside a ruler, and keep the raw load readings. If the legs look uneven, review the hole size and setting stroke before changing the rivet.
China Top Custom Aluminum Tri-Fold Blind Rivets: Which Tests Measure Pull Force, Shear Strength, and Leg Deployment?
How to read: A value of 1 means the test directly assesses that property; 0 means it is not the test’s primary measurement. Axial tensile testing measures pull force, shear testing measures resistance to transverse loading, and installation inspection checks whether the rivet legs deploy and form correctly. Actual strength results depend on rivet size, material, grip range, and test setup.
How to Assess Chinese Suppliers: ISO 9001, Custom Tooling, and QC Records
When assessing Chinese suppliers of custom aluminum tri fold blind rivets, treat ISO 9001 as a starting point, not a guarantee. ISO’s 2022 Survey recorded more than 1.26 million ISO 9001 certificates worldwide, showing how widely the system is used. Ask for the supplier’s current certificate, its site address, and the scope covering manufacturing. Paper is not proof. Review how nonconforming batches are isolated and how corrective actions are documented.
Custom tooling affects fit and consistency. Ask who owns the dies, how wear is checked, and whether tool changes require your approval. Request a sample run using your drawing, then compare grip range, head dimensions, and setting performance. Good suppliers can explain their inspection method, not just promise “tight tolerances.” Details matter.
QC records should connect measurements to a real production lot. Request a recent, anonymized inspection report, material certificate, calibration status, and records of pull-out or setting tests where applicable. Check that the report identifies the batch, sample size, acceptance limits, and actual results. A polished spreadsheet can still hide weak sampling. I would also ask what happens when a result falls outside specification; that answer often reveals more than a certificate.